

- Home
- Product
- About Us
- Lost Foam Casting Process
- Lost Foam Casting Video
- Success Case
- Contact Us


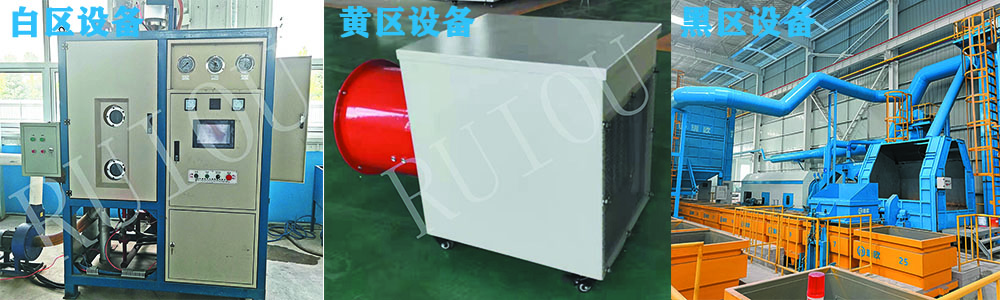
If you are trying to understand the evaporative pattern casting process, the most important question is usually not “What is lost foam casting?” but “How does material actually move from raw metal to a stable casting without hidden defects?” That question comes up in foundries dealing with lost foam casting line material flow, lost foam casting process steps, and evaporative pattern casting defects because the entire line depends on how well material is transferred, controlled, and vented at each stage. In practice, the workflow is a chain of foam molding, coating, drying, assembly, sand filling, pouring, and shakeout, and each link affects casting porosity control, metal fill behavior, and dimensional accuracy. Ruiou often explains this to buyers in a simple way: if the material flow is stable, the line produces repeatable castings; if it is not, the same line can generate scrap rates above 8% in one shift and under 2% in another.
This article answers the full user problem from start to finish: what equipment is needed, how the material travels through the line, what real production issues occur, and how operators can prevent waste. It is written for plant managers, process engineers, and purchasing teams who want a practical lost foam casting line setup guide, not a theoretical overview. You will also see a real-world case, measurable data, and professional process terms such as exothermic coating, negative pressure system, and sand compaction density so you can compare your line against industry practice.
Most people searching for a lost foam line are facing one of four problems:
The real intention behind the search is usually cost control. In foundry operations, even a 3% reduction in scrap can have a visible effect on monthly output because every rejected casting carries not only metal cost but also foam pattern, coating, sand handling, energy, and labor cost. When users ask about the lost foam casting process, they are usually trying to answer questions like these:
The best lines are designed around these pain points. Ruiou’s project experience shows that when the material flow is mapped properly, operators spend less time waiting, fewer patterns are damaged during transfer, and pouring stability improves because the mold is always ready when the metal arrives.
Before building or buying a complete line, you need to prepare four categories of resources: process data, equipment, materials, and personnel. A missing item in any one of these can create downtime on the first production run.
For example, in one Ruiou-supported project for a medium-sized iron casting plant, the team recorded that a stable coating layer in the range of 0.8 to 1.5 mm reduced surface defects compared with inconsistent manual dipping. The line also maintained a sand filling density difference of less than 2% between boxes, which helped reduce local collapse during metal replacement. These are not cosmetic details; in lost foam casting, they are process controls.
The material flow in a complete lost foam casting line follows a clear logic: foam becomes a pattern, the pattern becomes a coated assembly, the assembly becomes a sand-embedded mold, and the mold becomes a metal casting after pouring and vaporization. Below is the full process from the perspective of material movement and user operation.
The line begins with expandable polystyrene beads. These beads are fed into the pre-expander, where steam expands them to the required density. This stage determines the pattern’s final strength, surface quality, and dimensional stability.
Why this matters: if the bead density is too low, the foam pattern can collapse during handling. If it is too high, gas generation during pouring can rise and affect filling. In one production case involving ductile iron parts, a plant reduced foam breakage by changing bead density from an unstable manual setting to a controlled range that stayed within a narrow process window. Pattern breakage during transfer dropped from 6.4% to 1.9% over a 30-day trial.
The expanded beads are transferred to the molding machine, where they are fused into the exact shape of the required casting. This is the first place where dimensional accuracy is set. Mold temperature, steam pressure, cooling time, and fill stability all influence the result.
Material flow point: the beads must move evenly into the mold cavity. Uneven fill creates density variation, which later appears as warping or localized shrinkage after drying and handling.
After molding, the foam pattern is trimmed, inspected, and repaired. Operators check gate positions, surface dents, broken edges, and dimensional deviation. This is a small step, but it prevents large losses later.
In a real workshop case, a customer producing pump housings found that 70% of their rejected castings came from tiny pattern dents that were ignored before coating. Once they added a 100% visual inspection step and an edge repair station, first-pass yield increased by 11 percentage points within two weeks.
The foam pattern is dipped, sprayed, or brushed with a refractory coating. This coating performs two critical jobs: it supports the foam surface during pouring and allows generated gas to escape through controlled permeability.
Professional term note: coating viscosity, permeability, and refractoriness must be balanced. If permeability is too low, gas cannot escape and defects rise. If it is too high, metal penetration and rough surfaces may appear.
Ruiou often recommends measuring coating thickness instead of judging by eye. In one line, a coating thickness range of 1.0 to 1.2 mm produced a more stable surface finish than a hand-applied layer that varied from 0.6 mm to 2.0 mm across the same batch.
After coating, the pattern must enter the drying area. This step is often underestimated by new users. The coating must dry completely, because residual moisture can flash into steam during pouring and increase defect risk.
Material flow point: patterns move from wet to dry storage through a controlled air environment. If the transfer path is too long or humidity is high, the coating can absorb water again before assembly.
One customer case from a northern factory showed that moving coated patterns from an open staging area into a closed drying room reduced surface blister complaints by 43% in one quarter. The operator had not changed the alloy or pouring method, only the moisture control around the pattern flow.
Once dry, individual foam patterns are joined into a casting cluster with risers, runners, and gates. This stage decides how molten metal will travel through the cavity after pouring.
Why material flow here is critical: if the runner layout is poor, metal replacement becomes uneven. The gas from foam decomposition must exit while metal advances. A cluster that looks correct visually can still fail if the gating geometry creates dead zones.
In a Ruiou project for automotive counterweights, changing the cluster orientation improved fill consistency enough to reduce misrun defects by 28% over two months. That improvement came from revising material flow, not from changing the furnace.
The assembled foam cluster is placed in a flask or sand box, and dry sand is filled around it under vibration. Sand compaction is one of the most important process variables in the whole line.
Professional term: sand compaction density affects mold support, gas venting, and pattern deformation resistance. Dense enough sand supports the foam during pouring, but overly compacted sand can reduce gas escape paths.
Common industry practice is to monitor compaction consistency rather than only fill volume. In one measured case, a plant that controlled vibration time and fill rate reduced local collapse at thin-wall sections by 35%.
In many complete lost foam lines, a negative pressure system is applied to improve gas evacuation and stabilize the sand mold. The vacuum helps draw gases out as the foam vaporizes and the metal replaces it.
Material flow point: during this step, the system must remain stable. Pressure fluctuation can disturb metal movement and create partial fill defects. For users who ask why a line works in the morning and fails after lunch, unstable vacuum performance is often part of the answer.
The pouring stage is the point where the pattern disappears and the casting is formed. Molten metal enters the gating system, heats the foam, decomposes it, and occupies the space left behind.
Professional terms: pouring temperature, metal head pressure, and foam gasification rate must be matched. If pouring temperature is too low, the metal may not fully replace the foam. If too high, the coating and sand interface may suffer and increase burn-on or surface roughness.
A user case from an iron foundry showed that adjusting pouring temperature by 20 to 30°C within the alloy’s safe window reduced misruns in thin ribs by 17%. This is a good example of using data instead of guessing.
After pouring, the metal cools and solidifies inside the sand mold. The cooling rate influences shrinkage, grain structure, and internal stress.
In complete lost foam casting line material flow, cooling is not an isolated stage. It is the result of everything upstream: pattern density, coating permeability, sand compaction, and pouring speed. If the earlier flow was unstable, cooling defects often appear as delayed symptoms.
When the casting reaches the appropriate temperature, the box moves to shakeout. The sand is removed and sent to reclamation, while the casting proceeds to cleaning.
Material flow point: the reclaimed sand path matters because dust loading and grain degradation can affect the next production cycle. A clean sand loop can extend process stability, while a dirty loop often creates hidden variability in later batches.
The final step includes removing residual coating, gates, and flash, then inspecting the finished casting. Defects are classified, measured, and fed back into the process.
Plants that treat inspection data as part of the material flow tend to improve faster. A Ruiou client that logged defect location, sand batch, and coating lot number was able to trace repeated porosity to one drying rack position. After reassigning airflow in that zone, the defect frequency dropped from 4.8% to 1.6% in six weeks.
A midsize machinery foundry in Southeast Asia contacted Ruiou after struggling with inconsistent output from a complete lost foam casting line. Their main complaint was not that the equipment was broken, but that the process “looked fine” while the results kept changing. Scrap rate fluctuated between 5% and 11%, especially on parts with thin walls and long flow paths.
After a line audit, three issues were found:
Ruiou helped the plant standardize the material flow by adding coating thickness checks, a controlled drying room, and fixed vibration parameters. Over the next 60 days, the plant recorded:
The plant manager later said the biggest change was not a single machine, but the way material moved through the line. That is the real lesson of lost foam casting: line performance comes from flow stability, not isolated equipment strength.
Cause: low bead density, rough handling, or long waiting time before coating.
Solution: keep density within a fixed process range, shorten transfer distance, and use dedicated pattern racks.
Cause: coating still contains moisture or permeability is too low.
Solution: verify drying time with a moisture check, and test coating permeability instead of relying only on touch.
Cause: poor gating design, low pouring temperature, or unstable vacuum.
Solution: review runner layout, confirm temperature window, and monitor negative pressure continuously during pouring.
Cause: insufficient sand compaction or inconsistent vibration.
Solution: set vibration time standards and measure compaction density by batch.
Cause: no standardization of process parameters.
Solution: use a shift record sheet for coating thickness, drying time, sand filling time, and pouring temperature. Ruiou recommends treating these as control points, not casual notes.
A complete lost foam casting line is not just a set of machines. It is a controlled material flow system where foam, coating, sand, vacuum, and molten metal each move in the right sequence and under the right parameters. If one stage is unstable, the defect often appears several stages later, which is why many users feel the process is “hard to control” even when the equipment seems advanced.
If you are planning a new line, start by mapping the material flow before selecting machines. Confirm your target alloy, expected output, coating performance, drying conditions, and sand recovery strategy. If you already have a line, track your process data by batch and compare it across shifts. In most cases, the fastest gains come from stabilizing coating, drying, and sand compaction before changing major equipment.
Ruiou’s practical advice is simple: choose a line that supports traceable process control, not just one that looks complete on paper. A line that produces 500 stable castings per day is more valuable than one that can theoretically produce 700 but only does so on a good shift. In lost foam casting line material flow, consistency is the true output.
It is a casting method where a foam pattern is coated, embedded in dry sand, and then replaced by molten metal during pouring. The foam evaporates or decomposes, leaving the final casting shape.
Material flows from foam beads to molded patterns, then to coated and dried assemblies, then into sand-filled molds, and finally into the pouring, cooling, shakeout, and reclamation stages.
Common defects include gas porosity, misrun, sand collapse, burn-on, and dimensional deviation. Many of these are linked to coating, drying, and vacuum control.
Standardize pattern density, coating thickness, drying time, sand compaction, and pouring temperature. Also record each batch so defect trends can be traced back to the source.
Ruiou provides practical support for complete lost foam casting line planning and process optimization, especially for buyers who need stable material flow and consistent output rather than isolated machinery.
If you want a high-yield lost foam casting line setup guide, stable cast surface quality, and lower porosity control risk, the key is to manage every transfer point in the evaporative pattern casting process with measurable standards, not assumptions.
Previous: None


Copyright © Hebei Ruiou Intelligent Equipment Co., LTD. All Rights Reserved. | Sitemap | Powered by