

- Home
- Product
- About Us
- Lost Foam Casting Process
- Lost Foam Casting Video
- Success Case
- Contact Us


RUIOU provides integrated lost foam casting molding equipment as part of complete lost foam casting production lines. The Black Area system combines sand filling, vibration compaction, molding flasks, negative pressure control, casting operations, flask handling, and turnover equipment to support a coordinated molding process.
Unlike purchasing individual molding machines, an integrated Black Area system must be configured according to casting dimensions, flask capacity, molding cycle, vacuum requirements, and sand circulation capacity. RUIOU supplies complete lost foam casting production lines rather than standalone machines, ensuring that Black Area equipment is selected in coordination with the entire casting process.
For the complete production system, explore ourlost foam casting equipment and production line solutions.
The Black Area integrates several equipment groups, each performing a specific function during sand molding and casting. Equipment selection should consider the entire operating sequence rather than the capacity of a single machine.
| Equipment System | Available Equipment | Main Function |
|---|---|---|
| Sand Filling | Sand Storage Hopper, Movable Shower Type Sand Feeder | Supply and distribute dry molding sand around foam pattern clusters. |
| Vibration Compaction | Fixed, Movable, Airbag, Three-Dimensional, and Suspension Excitation Vibration Tables | Compact molding sand around foam patterns and complex geometries. |
| Molding Flasks | Lost Foam Casting Sand Boxes | Contain foam patterns and dry sand while supporting vacuum molding. |
| Negative Pressure | Vacuum Pump System, Negative Pressure Distributor, Vacuum Piping | Provide and distribute negative pressure during the casting process. |
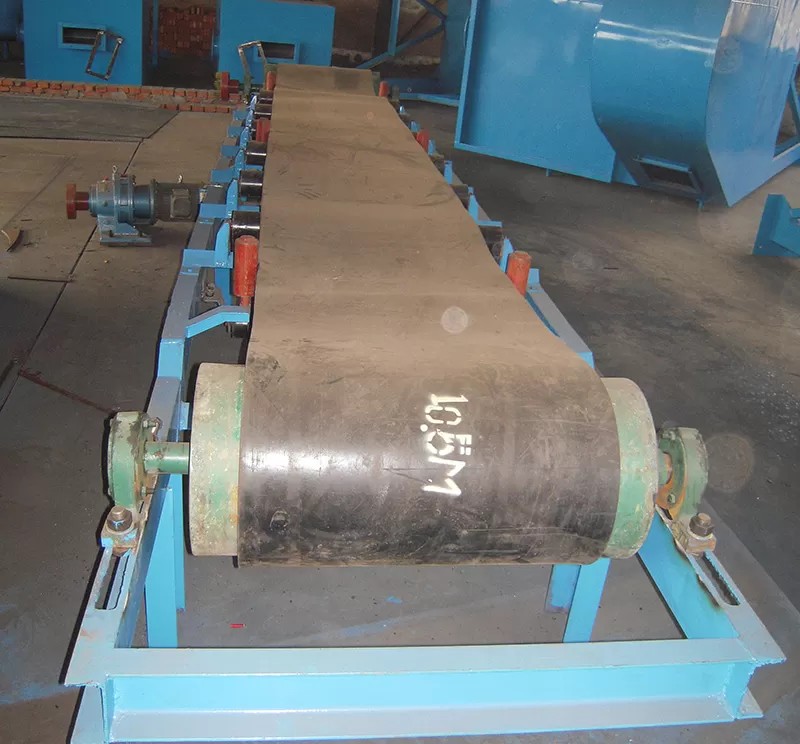
| Flask Handling | Transfer Equipment and Bottom Flip Hydraulic Turnover Machine | Transfer flasks between operations and discharge sand after the required cooling period. |
| Dust Collection | Impulse Bag-Type Dust Remover and Related Dust Collection Equipment | Collect dust generated during selected sand handling and processing operations. |
| System Controls | Electrical Controls, Automatic Interfaces, and Optional PLC-Based Coordination | Coordinate equipment movements and operating sequences. |
Sand cooling, screening, magnetic separation, and extended material conveying are coordinated with thesand processing system.
RUIOU's product catalog presents two automatic lost foam casting production line designs. The following figures are published line-level reference configurations, not interchangeable ratings for individual molding equipment.
| Technical Parameter | 5,000 t/year Reference Line | 10,000 t/year Reference Line |
|---|---|---|
| Annual Casting Capacity | 5,000 tonnes/year | 10,000 tonnes/year |
| Reference Molding Rate | 10 flasks/hour | 18 flasks/hour |
| Associated Melting Capacity | 2 tonnes/hour | 4.5 tonnes/hour |
| Sand Treatment Figure Published in Catalog | 17 m³* | 26 m³* |
| Production Arrangement | Integrated automatic casting line | Integrated automatic casting line |
| Molding Operations | Sand filling, molding, pouring, cooling transfer, and turnover | Sand filling, molding, pouring, cooling transfer, and turnover |
| Production Line Integration | White Area, Yellow Area, Black Area, and supporting sand processing | White Area, Yellow Area, Black Area, and supporting sand processing |
| Parameter | Published RUIOU Capability | Optional / Custom Range |
|---|---|---|
| Molding System Type | Integrated lost foam casting Black Area equipment | Semi-automatic, automatic, and project-specific arrangements |
| Annual Line Capacity | 5,000 and 10,000 tonnes/year reference configurations | Other capacity targets according to casting conditions and engineering design |
| Molding Rate | 10 and 18 flasks/hour reference line configurations | Approximately 5–20 flasks/hour configurations |
| Flask Length | Selected according to the production line | 1,000–2,000 mm conventional reference sizes; larger configurations up to approximately 3,100 mm |
| Flask Width | Selected according to the production line | 630–1,600 mm conventional reference sizes; larger configurations around 1,900–2,000 mm |
| Flask Height | Determined by casting and pattern requirements | Different flask heights and special structures according to project requirements |
| Vacuum Pump Series | SK-20, SK-30, 2BE-252, 2BE-253 series | Different pump combinations and distribution arrangements |
| Common Vacuum Exhaust Capacity | 20, 25, 35, and 43 m³/min published values | System capacity calculated according to simultaneous vacuum demand |
| Operating Negative Pressure | No universal operating range specified | Process-specific vacuum setting; approximately -0.04 to -0.06 MPa may be evaluated where technically appropriate |
| Vibration Equipment | Multiple fixed, movable, airbag, and suspension vibration structures | Customized platform dimensions, loading capacity, vibration parameters, and clamping arrangements |
| Sand Filling | Sand storage and shower feeding equipment | Custom feeding volume, station arrangement, and material flow |
| Flask Turnover | Bottom Flip Hydraulic Turnover Equipment | Customized flask load, turnover structure, and handling interfaces |
| Control System | Integrated automatic line configurations | PLC, HMI, automatic transfer, monitoring, and control interlocks |
| Electrical Supply | Determined by project equipment specifications | Voltage and frequency adapted to the installation country |
| System Layout | Integrated Black Area line arrangement | Customized station layout, handling route, and factory interfaces |
Molding flask dimensions affect pattern arrangement, sand consumption, vibration load, vacuum demand, and handling equipment.
| Flask Plan Dimensions | Configuration Category | Selection Considerations |
|---|---|---|
| 1000 × 800 mm | Compact reference configuration | Smaller pattern clusters and compact station layouts |
| 1200 × 1200 mm | Conventional reference configuration | General-purpose casting cluster arrangements |
| 1200 × 1400 mm | Conventional reference configuration | Medium-size clusters and flexible molding layouts |
| 1750 × 1600 mm | Larger conventional configuration | Larger casting clusters requiring increased flask space |
| 2000 × 1600 mm | Large custom reference configuration | Large casting or cluster layouts |
| 3100 × 1900 mm | Special large-format reference configuration | Project-specific oversized molding applications |
RUIOU provides several vibration equipment structures for lost foam casting molding systems. The suitable design depends on the molding flask, pattern geometry, required sand filling performance, and production line arrangement.
| Vibration Equipment Type | Structural Characteristics |
|---|---|
| Fixed Vibration Table | Stationary vibration platform integrated into a molding station |
| Movable Vibration Table | Movable vibration equipment arrangement |
| Three-Dimensional Vibration Table | Vibration arrangement capable of multi-directional sand compaction |
| Suspension Excitation Vibration Table | Suspended excitation structure |
| Airbag Vibration Table | Airbag-supported vibration equipment |
| Embrace-Clamp Vibration Table | Clamping structure used to secure the molding flask |
The negative pressure system is a critical part of lost foam casting molding equipment.
| Technical Item | Available Configuration | Selection Requirement |
|---|---|---|
| Vacuum Pump Series | SK-20, SK-30, 2BE-252, 2BE-253 | Choose according to required airflow and system operating conditions. |
| Published Common Exhaust Capacities | 20 / 25 / 35 / 43 m³/min | Calculate the required total extraction capacity before selecting the pump arrangement. |
| Negative Pressure Distribution | Manual and automatic connection arrangements | Select according to line automation, flask movement, and connected stations. |
| Vacuum Network | Piping, distribution devices, and associated system components | Account for pipe resistance, leakage, and simultaneous vacuum demand. |
| Operating Pressure | Defined by the casting process | Confirm target gauge pressure and control requirements during engineering. |
| Control Functions | Equipment control and optional automated distribution | Define pressure monitoring, operating sequences, and control interlocks. |
Automation can improve coordination between molding stations
| Process Stage | Semi-Automatic Arrangement | Customization |
|---|---|---|
| Sand Filling | Mechanized filling with operator participation | Feed rate, station quantity, and feeding interface |
| Vibration Compaction | Equipment-assisted vibration with operator-controlled sequences | Cycle logic, vibration settings, and flask handling |
| Vacuum Connection | Manual or assisted connection | Connection interface, distribution, and pressure monitoring |
| Flask Transfer | Mechanized transfer with operator involvement | Track layout, transfer stations, and operating sequence |
| Flask Turnover | Hydraulic turnover with manual operation | Flask dimensions, load, and turnover cycle |
| System Monitoring | Local equipment controls | Alarm logic, interface requirements, and operating data |
The selection of an automatic system should be based on the required equipment functions and production sequence. Not every automatic production line requires the same handling equipment or control architecture.
RUIOU supports customized Black Area configurations within complete lost foam casting production line projects. Custom engineering covers mechanical dimensions, operating capacity, equipment arrangement, control interfaces, and coordination with the sand processing system.
| Custom Item | Available Customization |
|---|---|
| Molding Flask | Length, width, height, structural reinforcement, sealing, and vacuum interfaces |
| Vibration System | Platform dimensions, rated load, supporting structure, vibration arrangement, and controls |
| Vacuum System | Pump arrangement, airflow capacity, distribution network, and operating control |
| Sand Filling | Feeding equipment, storage capacity, distribution arrangement, and station positioning |
| Turnover & Transfer | Flask handling capacity, transfer arrangement, turnover interface, and equipment layout |
| Automation | Equipment coordination, PLC-based functions, HMI, interlocks, and handling sequences |
| Electrical Configuration | Voltage, frequency, electrical components, and control interfaces |
| Equipment Finish | Industrial protective finishes and project-specific coating requirements |
| Workshop Layout | Equipment placement, material flow, transfer stations, and system interfaces |
No. RUIOU supplies molding equipment as part of complete lost foam casting production lines. The molding system, vacuum equipment, flask handling, and sand processing equipment are configured together for an integrated project.
RUIOU's published automatic production line reference designs include 10 flasks/hour and 18 flasks/hour configurations, associated with 5,000 and 10,000 tonnes/year line designs. Other molding rates can be configured according to the required capacity, flask dimensions, and process conditions.
Yes. RUIOU can configure molding flasks according to casting dimensions and production requirements. Conventional reference dimensions include 1000 × 800 mm, 1200 × 1200 mm, and 1200 × 1400 mm, while larger project-specific configurations can include dimensions around 3100 × 1900 mm. Final height, load, and structural design require engineering confirmation.
The vacuum system is selected according to simultaneous flask demand, vacuum piping, system leakage, and casting process requirements. RUIOU publishes common exhaust capacities of 20, 25, 35, and 43 m³/min.
Yes. RUIOU provides integrated automatic production line configurations with coordinated sand filling, vibration, vacuum connection, transfer, and turnover functions. The exact degree of automation depends on production requirements and the approved equipment scope.
A Black Area system can be designed around an existing building where the required equipment, handling space, utilities, foundations, and safe operating conditions can be accommodated. Provide the workshop layout, clear height, column locations, and planned production capacity for evaluation.
Selecting the right lost foam casting molding equipment requires more than choosing a vibration table or vacuum pump. Flask dimensions, molding efficiency, sand circulation, vacuum capacity, and automated handling must work together to achieve the required production output.
RUIOU provides complete lost foam casting production line solutions with integrated Black Area molding systems. Whether you are planning a new foundry or expanding an existing production facility, share your casting drawings, target annual capacity, preferred automation level, and workshop conditions. Our team can review the project requirements and discuss a suitable equipment configuration and production line quotation.


Copyright © Hebei Ruiou Intelligent Equipment Co., LTD. All Rights Reserved. | Sitemap | Powered by