

- Home
- Product
- About Us
- Lost Foam Casting Process
- Lost Foam Casting Video
- Success Case
- Contact Us


When you ask “What Data Is Needed to Size a Pneumatic Sand Conveying System?”, you are really asking how to match airflow, pipe diameter, pressure, and feeder capacity to the exact sand-handling duty in your plant. In simple terms, a pneumatic sand conveying system moves dry sand through enclosed pipelines using air instead of belts or buckets, which helps reduce dust, improve cleanliness, and stabilize production. For foundries, this is not just a technical choice—it directly affects throughput, energy cost, maintenance frequency, and product quality. A correctly sized foundry sand pneumatic conveyor can prevent plugging, reduce wear, and keep molding lines supplied without interruption, creating measurable business value from day one.
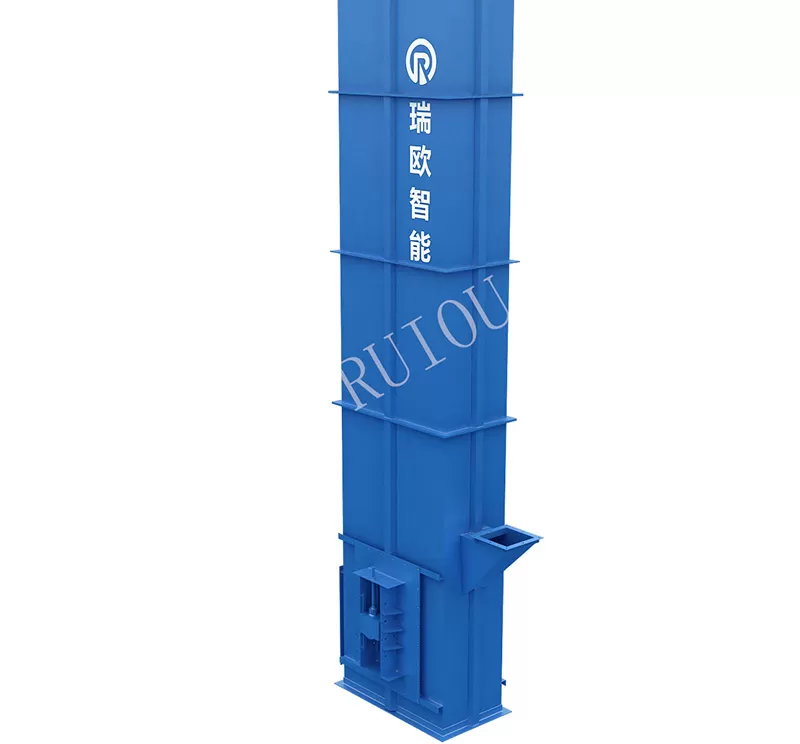
In modern foundry operations, sand is no longer treated as a low-value bulk material. Core shops, molding lines, reclamation units, and storage silos all depend on consistent sand transport. As production became more automated, the need for a reliable foundry sand pneumatic conveyor increased sharply, especially in plants where dust control and floor-space efficiency matter.
Ruiou has positioned itself around this practical requirement: designing conveying solutions based on process data rather than guesswork. In pneumatic conveying, “close enough” often becomes expensive. A pipe that is undersized can cause saltation, excessive velocity, and abrasion; a system that is oversized can waste compressed air and increase capital cost. This is why engineering teams insist on measured inputs, not rough estimates.
For a properly engineered pneumatic conveying system for sand, the sizing workflow is built around real process conditions, material behavior, and line layout. That is the difference between a stable system and a chronic maintenance issue.
Pneumatic conveying has been used for decades across cement, grain, chemical, and metalcasting industries. In foundries, the shift accelerated as plants sought enclosed transfer routes to reduce silica dust exposure and improve housekeeping. Over time, the foundry sand pneumatic conveyor evolved from a simple material-moving tool into a process-critical system integrated with silos, hoppers, classifiers, mixers, and reclamation loops.
Historically, many plants relied on mechanical conveyors or manual handling. These methods worked, but they created barriers: dust leakage, limited routing flexibility, and higher contamination risk. Pneumatic systems solved many of those issues by using pressure or vacuum to move sand through pipelines. Yet the success of the system depends on a disciplined engineering basis. That is why sizing data has become the foundation of every serious foundry sand pneumatic conveyor project.
To size a pneumatic conveying system for sand accurately, engineers need a complete set of process, material, and layout data. Missing even one key variable can distort the design. The following inputs are essential.
The sand itself drives most of the design decision.
Important data includes:
For foundry applications, silica sand, olivine sand, chromite sand, and reclaimed sand each behave differently. A foundry sand pneumatic conveyor for reclaimed sand may need different velocity control than one handling new dry silica sand. If the sand contains fines or binders, the conveying regime can shift toward more difficult flow behavior.
The engineer must know how much sand must be moved per hour or per minute.
You should define:
For example, a plant may need 12 t/h during normal operation but 18 t/h at peak pour preparation. If the system is sized only for the average load, the foundry sand pneumatic conveyor may fail during surge periods.
Line length and geometry strongly influence pressure drop.
Data needed:
A short, straight run behaves very differently from a long line with multiple 90-degree elbows. In a pneumatic conveying system for sand, each bend increases resistance and wear risk. This is why layout drawings matter as much as process numbers.
The system architecture must be defined early.
Common choices include:
For abrasive foundry media, dense phase may reduce pipe velocity and wear in some cases, but it is not universally better. The right choice depends on material characteristics and required throughput. Many plants specify a foundry sand pneumatic conveyor without first deciding whether the duty favors pressure or vacuum, which leads to design mismatch.
Air is the energy source of the system, so its quality and quantity are critical.
Needed inputs:
Compressed air inefficiency is one of the biggest operating costs. A pneumatic conveying system for sand that is under-supplied will lose conveying stability; one that is over-supplied may waste energy and increase pipe velocity beyond acceptable limits.
How sand enters and exits the line affects the entire design.
Relevant data:
A foundry sand pneumatic conveyor must coordinate feeding and discharge carefully. If the feeder cannot meter the sand consistently, the conveying line will experience slugging or instability.
The environment influences reliability and safety.
Consider:
Foundries are harsh environments. Heat, fine dust, vibration, and long operating hours demand robust design. A foundry sand pneumatic conveyor in a high-duty cast house must be engineered for wear and serviceability, not just theoretical capacity.
Reliable suppliers document performance against standards and inspection protocols.
Typical references may include:
These numbers matter because a pneumatic conveying system for sand is only as dependable as the process discipline behind it. Quality documentation and testing improve trust, reduce start-up risk, and support long-term maintenance planning.
When a customer approaches Ruiou for a foundry sand pneumatic conveyor, the engineering team typically gathers the following information before final selection:
| Data Category | Required Input | Why It Matters |
|---|---|---|
| Material | Bulk density, PSD, moisture, abrasiveness | Determines conveying behavior and wear |
| Capacity | t/h, batch size, peak demand | Sets line size and air demand |
| Distance | Horizontal/vertical length, bends | Affects pressure drop |
| System type | Pressure/vacuum, dilute/dense phase | Defines operating logic |
| Air supply | Pressure, flow, dew point | Impacts stability and energy use |
| Feed/discharge | Hopper, blow tank, receiver details | Controls material entry/exit |
| Environment | Temperature, dust class, duty cycle | Influences reliability and safety |
| Standards | ASTM, DIN, plant specs | Supports compliance and verification |
This checklist helps prevent the common mistake of starting with equipment selection before the process data is complete.
A foundry sand pneumatic conveyor is not sized by one number alone. Instead, it is the result of a chain of engineering decisions.
If sand is coarse and highly abrasive, the line velocity may need to be controlled to reduce elbow erosion.
If moisture is higher than expected, the system may suffer from buildup and reduced flowability.
If the conveying distance includes multiple risers and bends, the pressure demand increases quickly.
If the plant needs continuous operation, downtime risk becomes a primary design factor.
This is why experienced engineers treat every pneumatic conveying system for sand as a custom application. Even two plants producing similar castings may require completely different pipe diameters and blower capacities.
Many project delays begin with incorrect assumptions. The most common mistakes include:
This is false. Reclaimed sand, green sand, and dry new sand behave differently. Particle shape, fines content, and moisture all change the conveying profile. A foundry sand pneumatic conveyor must be matched to the actual material, not a generic sand category.
Also false. Excess velocity can increase erosion, energy cost, and segregation. In some cases, it can worsen pipe wear without improving stability. A well-designed pneumatic conveying system for sand targets the minimum reliable conveying velocity, not the maximum possible one.
Capacity is important, but it is not enough. Without routing data, air data, and feeder design, the system may fail in practice. A foundry sand pneumatic conveyor built only around throughput may still plug, overheat, or erode prematurely.
Not true. Dust control is part of the system performance. Poorly managed filtration can create backpressure, contamination, or emissions issues. In regulated facilities, the dust collection stage is essential to the entire pneumatic conveying solution.
Consider a foundry that needs to transfer 8 t/h of reclaimed silica sand from a reclamation unit to a storage silo 42 meters away, with 11 meters of lift and four elbows.
If the engineering team only knows the tonnage, it may choose a pipe diameter based on guesswork. But when the full data set is available—bulk density, moisture below 0.5%, particle size range, compressor pressure, and duty cycle—the design can be tuned more precisely.
In this example, the foundry sand pneumatic conveyor may require:
This is where Ruiou’s engineering approach adds value. By capturing the complete process data early, the company can reduce trial-and-error during commissioning and support a smoother startup. For many plants, that can mean fewer stoppages, lower compressed-air waste, and a cleaner transfer path.
A mid-sized casting plant once experienced recurring blockages in its foundry sand pneumatic conveyor during peak shifts. The root cause was not the pipework alone. The issue was incomplete sizing data: the project had ignored reclaimed sand fines, seasonal humidity changes, and the actual bend count in the final route.
After the line was re-evaluated using full material and routing data, the revised pneumatic conveying system for sand used improved feeder control, adjusted air supply, and wear-resistant elbows. The result was more stable operation and a significant reduction in unplanned shutdowns.
The lesson is straightforward: accurate data is cheaper than repeated downtime.
To speed up the design process, prepare these items in advance:
With this information, Ruiou can evaluate the project more accurately and recommend a suitable foundry sand pneumatic conveyor configuration.
The answer to What Data Is Needed to Size a Pneumatic Sand Conveying System? is clear: you need material properties, required capacity, conveying distance, system type, air supply data, feeder and discharge details, and operating conditions. For foundries, this is especially critical because sand is abrasive, process-sensitive, and central to production stability.
A properly engineered foundry sand pneumatic conveyor improves cleanliness, supports productivity, and lowers the risk of costly failures. If you are planning a pneumatic conveying system for sand, start with accurate data, verify standards, and demand documented testing. That is the most reliable path to long-term performance.
For more technical guidance or project support, Ruiou can help evaluate your process and build a system based on real operating conditions, not assumptions.


Copyright © Hebei Ruiou Intelligent Equipment Co., LTD. All Rights Reserved. | Sitemap | Powered by