

- Home
- Product
- About Us
- Lost Foam Casting Process
- Lost Foam Casting Video
- Success Case
- Contact Us


A molding sand belt conveyor is one of the most practical tools in modern foundry material handling. In casting plants, sand must move from mixing to molding, cooling, and reclamation without delay. If the line is not smooth, workers may face sand spill, dust, bottlenecks, and unstable mold feeding. That is why many plants now compare the Foundry Sand Belt Conveyor, molding sand conveyor system, and foundry sand transfer conveyor before they build or upgrade a line. A good layout can cut manual handling, reduce downtime, and keep sand flow stable from start to finish.
In many foundries, the problem is not only moving sand. The real issue is moving it at the right angle, at the right speed, and with the right dust control. For example, in a medium-size plant handling 20–50 tons of sand per hour, a poorly designed conveyor path can create extra transfer points, which often increase spillage and cleaning time. By contrast, a well-planned foundry sand belt conveyor line can simplify the route, reduce intermediate lifting, and improve overall material flow efficiency by a measurable margin.
If you are looking for a molding sand belt conveyor for foundry layout, a sand transfer conveyor for molding line, or a custom foundry sand conveyor system, the key is not just the machine itself. The key is how well it fits your plant layout, process rhythm, and dust control needs.

A foundry sand belt conveyor is a conveyor system that uses a moving belt to transport molding sand, reclaimed sand, core sand, or mixed sand between process stages.
In simple terms:
In foundry engineering, the belt conveyor is often chosen because it can handle:
According to conveyor engineering principles used in bulk material handling, belt conveyors are favored when a plant needs steady flow and lower operating cost per ton. Industry reports from major conveyor manufacturers and bulk handling technical guides show that belt conveyors often cost less to run than repeated forklift or bucket transfer for continuous material movement, especially in high-frequency foundry lines.
Sand is not a light material in daily production. It is abrasive, dusty, and often hot after reclamation. A foundry conveyor must therefore be designed for:
That is why the term molding sand belt conveyor is not just a piece of equipment name. It is a process tool that affects plant efficiency, cleanliness, and mold quality.
The best conveyor is the one that matches your layout. A foundry does not need the same system as a mine, warehouse, or food factory.
If your molding room, mixing area, and reclamation section are in one straight path, a foundry sand belt conveyor is often the best choice.
Why it works:
This layout is common in small and medium foundries. A straight conveyor route can reduce unnecessary handling and simplify plant planning.
Many workshops do not have enough space for a straight line. In that case, an L-shaped route with one or more belt conveyor sections is more practical.
Benefits:
A custom molding sand belt conveyor works well here because the belt length, angle, and discharge point can be adjusted.
Some foundries separate sand storage, mixing, and molding across different levels. For these plants, a belt conveyor with incline sections or a combined conveyor system is often needed.
Best use cases:
In this type of system, the conveyor design must consider belt slip, angle limit, and load capacity. For bulk materials, incline belt performance often depends on the sand’s angle of repose and belt surface friction.
If your plant has serious dust problems, you should not choose an open conveyor without protection.
Instead, look for:
This setup helps reduce airborne particles and improves workshop cleanliness. According to industrial dust control guidance, enclosed transfer points can significantly lower dust release during material movement when compared with open discharge.
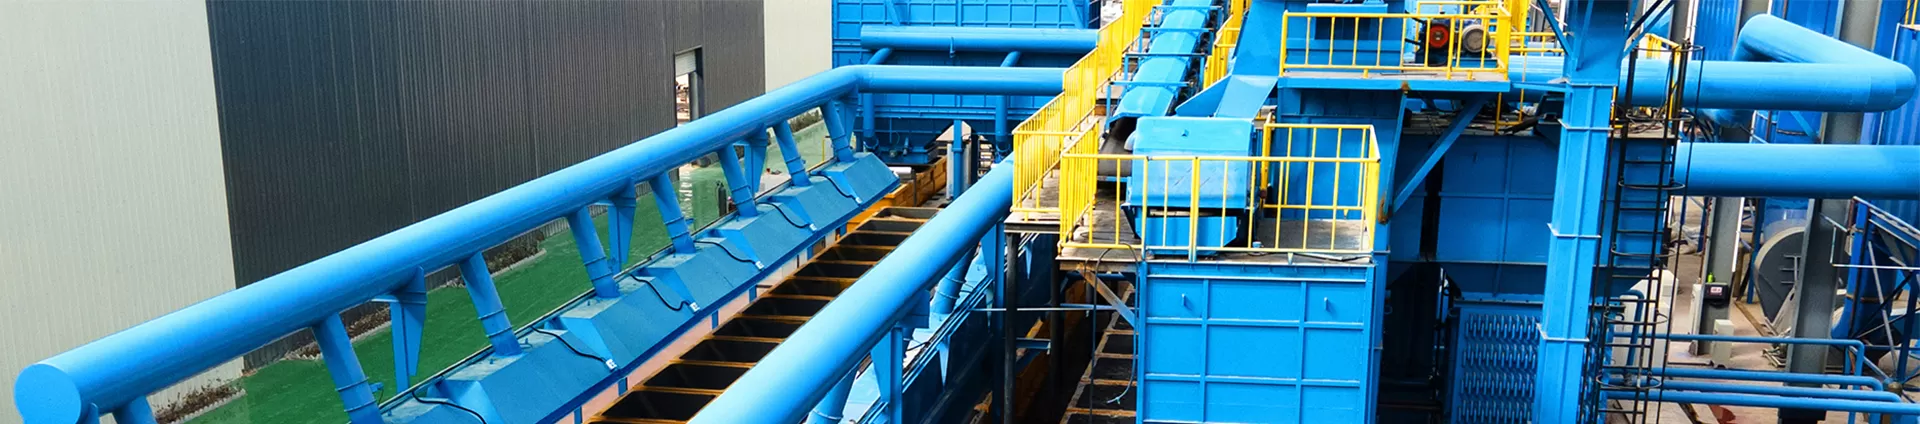
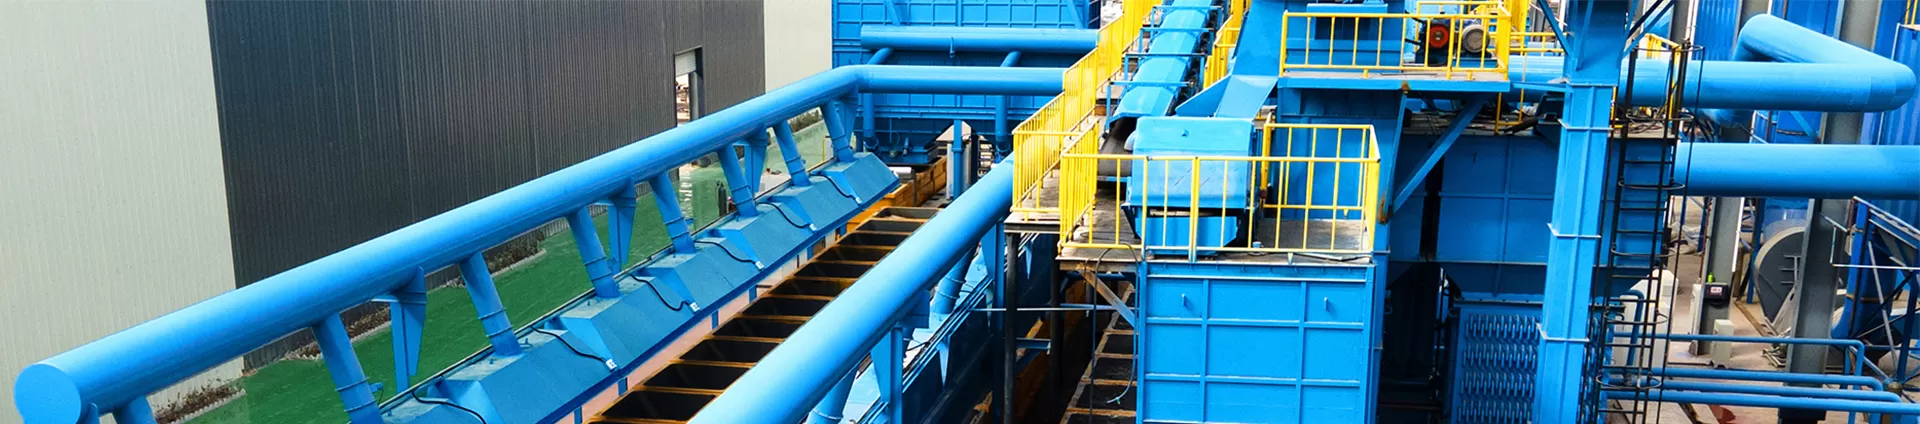
Below is an image that can help you understand the use of a foundry sand belt conveyor in a real layout.
Use this image to compare how the conveyor route fits different plant structures, especially when planning a molding sand belt conveyor for foundry layout or a sand transfer conveyor for casting workshop.
The main value of a molding sand belt conveyor is not only speed. It is process stability.
Manual sand handling is slow and tiring. In a typical foundry, workers may need to move sand many times per shift. A conveyor can replace repeated lifting, pushing, and shoveling. This helps reduce labor intensity and improves consistency.
Casting lines usually run best when sand supply is stable. If the sand feed stops, molding stops too. A belt conveyor keeps the flow steady and helps avoid line interruptions.
Sand spills may look small, but over a month they can become a large hidden cost. Better transfer design can reduce waste, cleaning time, and floor contamination.
Dust, scattered sand, and repeated manual handling all increase workplace risk. A good conveyor route helps keep aisles clear and lowers slip hazards.
In bulk handling systems, stable conveyance often improves overall throughput. For example, if a foundry reduces transfer interruptions and cleaning time, total line uptime can improve by measurable hours per month. That is more valuable than just “faster transport.”
A foundry sand belt conveyor can be used in many parts of the foundry process.
After fresh sand, binder, and additives are mixed, the conveyor can carry the material to the molding section.
The conveyor can deliver sand to molding machines at a stable rate.
After shakeout and cooling, reclaimed sand can be sent back to storage or reprocessing equipment.
Large sand bins or silos can discharge sand directly onto a conveyor for automatic feeding.
Used sand can also be transported to disposal or treatment areas.
In automated foundries, the conveyor can connect mixers, hoppers, elevators, cooling systems, and molding stations into one flow.
For plants with frequent material movement, a molding sand belt conveyor system is often a core part of the process, not just an accessory.
The importance of a conveyor becomes easier to understand when you look at measurable benefits.
Compared with repeated manual handling, a conveyor usually reduces labor needs and handling time. In many industrial plants, continuous conveying is preferred because the cost per ton can be more predictable than intermittent transport methods.
Consistent belt speed helps stabilize feeding. This matters because uneven sand supply can affect mold quality and line rhythm.
Each extra transfer point creates a chance for loss. A direct conveyor route can reduce these points.
A belt conveyor can connect different equipment types, such as mixers, bunkers, screens, and hoppers.
The system can be designed for straight, inclined, or combined routes. That flexibility is a major reason why many plants choose a custom foundry sand belt conveyor.
With covers, sealing, and local extraction, the conveyor can help control dust in the work area.
Before buying, ask these questions:
You need to know the hourly flow rate, not only daily output.
Longer routes may need stronger belt support and more careful drive selection.
If yes, you must check belt grip, angle limit, and anti-slip design.
If your workshop is dusty, choose covered conveyor sections and sealed transfer points.
Hot reclaimed sand and sharp particles may need wear-resistant belt materials and stronger rollers.
Small layouts often need compact or L-shaped conveyor designs.
A good system should leave room for extra lines or higher capacity later.
When comparing products, do not only look at price. Check the technical details.
Common options include:
Wider belts can carry more material, but they also need more space.
Belt speed must match sand type and flow rate. Too fast can increase spill; too slow can reduce output.
The drive motor must handle the load and incline.
A strong frame is important because foundry environments are harsh.
Side skirts, covers, and chute connections matter a lot in foundries.
Easy inspection points can reduce downtime.
To make this topic more reliable, it helps to compare with respected industry sources and technical guidance:
These sources support the main idea: the best conveyor is not the most expensive one, but the one that matches the material, route, and maintenance needs.
If you are planning a new foundry line or upgrading an old one, Ruiou can help you select a suitable foundry sand belt conveyor based on your layout, capacity target, and dust control needs.
You can further understand:
If your plant needs a molding sand belt conveyor for foundry production, a Ruiou foundry sand conveyor system, or a custom sand transfer conveyor for molding workshop, the next step is to review the technical drawing and operating guide before purchase.
A foundry version is designed for abrasive, dusty, and sometimes hot sand. It usually needs stronger wear resistance and better dust sealing.
Yes. Reclaimed sand is a common use case, but the belt and frame should be selected based on particle size, temperature, and moisture.
For many foundries, yes, especially when the goal is continuous and longer-distance transfer. A screw conveyor may be better for short, enclosed, or controlled feed points.
Use covers, skirt boards, proper chute design, and local dust extraction at transfer points.
A straight or L-shaped layout is often best because it saves space and reduces transfer points.
Base it on hourly sand demand, not just daily output. Also consider peak load and future expansion.
You can review the user guide, request a layout drawing, and ask Ruiou for a customized plan based on your workshop size and process flow.
If you are comparing the best sand conveyor for different foundry layouts, start with your plant map, sand flow rate, and dust control target. Then match those needs to the right foundry sand belt conveyor type.
The smartest next step is to:
A good conveyor is not just equipment. It is part of a stable casting process. When the sand flow is right, the whole foundry runs more smoothly.
If you want, I can also turn this into:
Previous: None


Copyright © Hebei Ruiou Intelligent Equipment Co., LTD. All Rights Reserved. | Sitemap | Powered by